Custom Lithium Ion Battery Pack: Howell Energy’s UL and IEC 62133 Certified OEM/ODM Services
SHENZHEN, GUANGDONG, CHINA, October 25, 2026 /EINPresswire.com/ -- Commercial equipment developers and electronic
Press Release Disclaimer: This is a press release distributed through the XPR Media network. It has not been independently verified by our newsroom.

SHENZHEN, GUANGDONG, CHINA, October 25, 2026 /EINPresswire.com/ — Commercial equipment developers and electronic device manufacturers require dedicated power architectures that fit tight mechanical envelopes. Modern procurement programs prioritize flexible OEM and ODM engineering, tailored PCM/BMS integration, and strict safety validation. Headquartered in Shenzhen with an advanced manufacturing base in Dongguan, Howell Energy Co., Ltd. specializes in complete custom lithium battery pack engineering. The company provides one-to-one technical development covering customized dimensions, terminal wiring, and smart communication protocols.
Deploying custom lithium battery packs into international commercial markets involves stringent technical and regulatory hurdles. Equipment developers must verify that cell geometries, protective circuitry, and outer enclosures integrate smoothly within host devices. To determine whether a manufacturer can support demanding OEM and ODM programs, project directors evaluate three core operational benchmarks:
In-House Engineering R&D and Custom BMS Development: Direct control over cell chemistry selection, 3D mechanical enclosure modeling, and proprietary BMS firmware integration.
Automated High-Precision Manufacturing and Multi-Stage QC: Automated electrode processing, precision laser micro-spot welding, and full-scale electrical screening across cell batches.
Complete Safety Compliance and Certification Readiness: Turnkey certification support for global market distribution, including UL 1642, UL 2054, IEC 62133, CE, and UN 38.3.
In-House Engineering R&D and Custom BMS Development
Turnkey battery customization begins with a detailed engineering evaluation to determine the optimal electrochemistry and topological layout. Howell Energy maintains dedicated R&D engineering teams specializing in electrochemistry, mechanical packaging, and electronic circuitry. Engineers evaluate customer requirements spanning nominal operating voltages, continuous current loads, physical space envelopes, and ambient operating temperatures.
Depending on physical constraints, Howell Energy selects from cylindrical 18650 and 21700 cells, prismatic aluminum cells, or ultra-thin lithium polymer pouches. Multicell configurations range from single-cell 3.7V units to 72V and 74V high-voltage modules. Circuit trace designs distribute high currents evenly across parallel cell branches, preventing localized resistance heating.
Mechanical design teams utilize 3D computer-aided modeling to build rigid internal structures. Structural engineers incorporate specialized cell holders, vibration dampers, and precision-cut silicone thermal interface pads. For compact enclosures, thermal dissipation channels guide heat away from internal electronic components. These structural techniques maintain stable internal temperatures during extended high-drain operations.
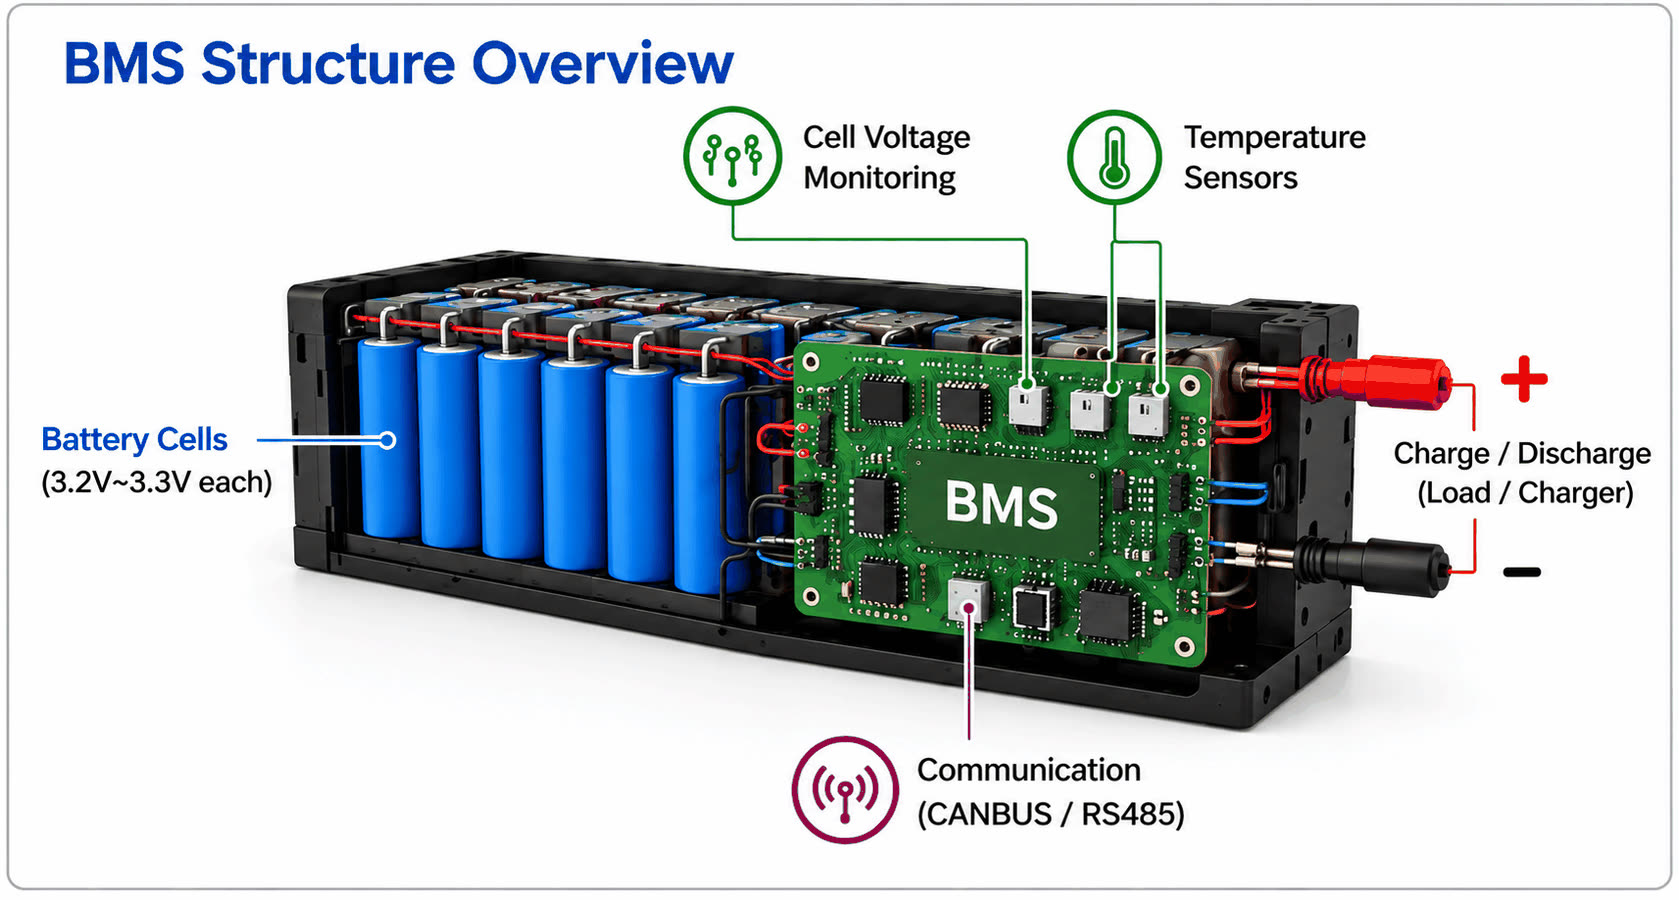
Electronic protection forms the core of every custom pack design. Howell Energy develops proprietary hardware and software Battery Management Systems tailored to client duty cycles. The BMS provides multi-stage protection against overcharge, deep overdischarge, continuous overcurrent, and short circuits, incorporating passive or active cell balancing to maintain voltage uniformity across extended cycle lives. Precision NTC thermistors monitor internal cell clusters, enabling multi-stage high- and low-temperature charge cutoffs alongside thermal warnings to prevent lithium plating and thermal runaway in extreme environments.
For smart equipment integration, engineers incorporate standard industrial communication protocols, including CANbus, RS485, SMBus, and UART. These digital interfaces transmit real-time state of charge, temperature tracking, and diagnostic telemetry to host system controllers. Integrated Coulomb-counting fuel gauges provide accurate runtime forecasting for critical medical and robotics applications. Custom status indicators and LCD screens offer convenient local diagnostics for field maintenance technicians.
Automated High-Precision Manufacturing and Multi-Stage QC
Transitioning from engineering prototypes to full-scale mass production requires advanced automated manufacturing facilities. Howell Energy operates specialized production bases in Dongguan and Jiangsu, equipped with automated coating, winding, and cell formation lines. Automated sorting machines grade each cell by discharge capacity, open-circuit voltage, and AC internal resistance.
Maintaining narrow cell grouping tolerances prevents electrical imbalances and extends overall pack operating longevity. Cell groups matched for custom packs maintain voltage tolerances within narrow millivolt bands and internal resistance deviations within milliohm limits. This rigorous screening standardizes discharge plateaus across all production batches, maintaining uniform energy delivery under heavy loads.
Internal pack assembly utilizes automated laser micro-spot welding machines to join high-purity nickel interconnects. Precision welding parameters deliver minimal electrical resistance and high mechanical tensile strength. Quality control personnel implement strict IQC, IPQC, and FQC inspection protocols across every manufacturing stage.
Automated end-of-line test systems verify electrical performance across complete production batches. Test stations evaluate real-time charge and discharge efficiency, BMS cutoff voltage precision, and overall insulation resistance. In addition, multi-channel thermal cameras monitor surface heat distribution during full continuous current loading cycles.
Completed battery packs undergo mechanical stress testing, including multi-axis vibration profiles and standard 1.2-meter drop protocols. External enclosures utilize flame-retardant ABS compliant with UL 94 V-0 standards or extruded aluminum alloy housings with anti-corrosion surface treatments. Sealed casing designs achieve IP65 or IP67 ingress protection, shielding internal cells against moisture and dust.
Complete Safety Compliance and Certification Readiness
International market distribution requires verified regulatory compliance and accredited safety testing documentation. Howell Energy manufactures all custom battery assemblies under an ISO 9001 certified quality management framework. The company maintains extensive experience preparing products for international electrotechnical safety standards.
Custom configurations strictly adhere to IEC 62133, the benchmark international standard validating mechanical, electrical, and thermal safety for portable equipment across European and international markets. For North American commercial distribution, Howell Energy engineers assemblies to comply with UL 1642 for baseline cell integrity and UL 2054 for comprehensive pack-level fault protection against overcurrent and thermal runaway. Accompanied by European CE directives, UKCA regulations, and RoHS compliance, this traceable documentation matrix eliminates costly testing bottlenecks and streamlines statutory approvals for OEM product launches.
Factory engineers assist clients through third-party regulatory certification workflows from initial design submission to testing approval. Howell Energy coordinates directly with accredited international testing laboratories to execute electrical, mechanical, and environmental stress trials. This collaborative engineering approach prevents compliance delays during new device qualification.
Global freight logistics require verified compliance with dangerous goods transport regulations. Howell Energy provides certified UN 38.3 test summaries, official Material Safety Data Sheets, and drop test validation reports. Products pass the complete UN 38.3 testing matrix, including thermal shock, altitude simulation, vibration, and external short-circuit evaluations. These compliance documents support air, ocean, and ground freight logistics under international shipping rules.
Direct factory certification support accelerates customer regulatory approvals and shortens international product launch timelines. Customers receive complete documentation packages, including electrical schematics, BMS firmware maps, and accredited test certificates. This documentation transparency simplifies third-party audits and customs clearance procedures, enabling rapid deployment across global commercial markets.
Partnering directly with Howell Energy provides original equipment manufacturers with four distinct operational advantages:
Broad Electrical Configuration Scope: Flexible engineering covers voltages from 3.7V to 72V and capacities from 100mAh to 100Ah, supporting high continuous discharge ratings.
Verified Global Regulatory Matrix: Certified manufacturing facilities deliver battery assemblies compliant with ISO 9001, UL 1642, UL 2054, IEC 62133, and CE.
Agile Prototyping and Fast Response: A one-piece sample MOQ pairs with dedicated engineering evaluations delivered within 12 hours.
Turnkey Sourcing and Flexible Logistics: Direct factory manufacturing removes distributor markups, supported by EXW, FOB, CIF, and door-to-door DDP freight.
Technical Consultation and Factory Documentation
Original equipment manufacturers and hardware engineering teams are invited to submit custom battery specification drawings and enclosure parameters to Howell Energy. Access OEM/ODM design support and direct factory quotation through the official international engineering portal: https://www.howellenergy.com/.
Howell Energy Co., Ltd.
Howell Energy
Visit us on social media:
LinkedIn
Facebook
YouTube
Legal Disclaimer:
EIN Presswire provides this news content “as is” without warranty of any kind. We do not accept any responsibility or liability
for the accuracy, content, images, videos, licenses, completeness, legality, or reliability of the information contained in this
article. If you have any complaints or copyright issues related to this article, kindly contact the author above.

Media gallery